
Rotary Air Lock Valves
Rotary Air Lock Valve Manufacturer & Supplier in Russia & CIS
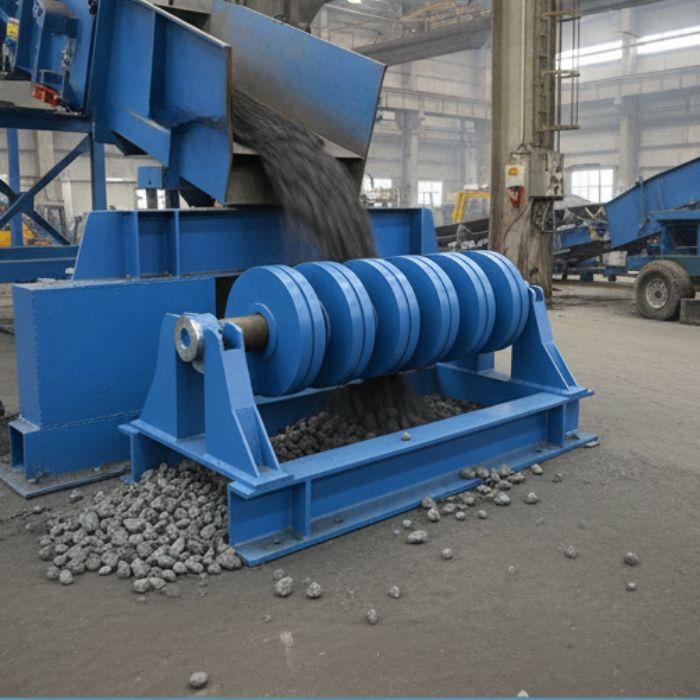
UGES designs and manufactures rotary air lock valves for reliable material metering and air sealing in pneumatic conveying and dust collection systems across Russia & CIS. Our valves feature precision-machined rotors with adjustable tip clearances, heavy-duty shaft seals, and robust CI/SS construction for handling cement, fly ash, food-grade powders, and abrasive materials. Every valve is tested to GOST R requirements and delivered with complete documentation.
Trusted by the largest brands
Russia & CIS Market Overview

Market Context

UGES Capability

Compliance Standards

Shipping Terms
Rotary Air Lock Valves Specifications for Russia & CIS
Rotor Diameter
Capacity Range
Operating Temperature
Drive Arrangement

Applications in Russia & CIS
Pneumatic Conveying Systems
Precision metering of cement, fly ash, andite powder into pneumatic pipelines with leakage rates below 0.5% at operating pressures up to 0.8 bar gauge.
Dust Collection Discharge
Continuous discharge of collected particulates from bag filters and ESPs with consistent volumetric feed rates, preventing air ingress into the collection system.
Food & Grain Processing
FDA-compliant stainless steel rotary valves for flour, sugar, and grain handling with quick-release end covers for easy cleaning and inspection.
What Our Partners Say
We have been sourcing material handling components from United Global Engineering Solutions for quite some time. Their conveyor accessories, including rollers and industrial pulleys, have consistently met our standards for quality and performance. We confidently recommend them for any conveyor system requirement.
Carlos MedinaRegular Client 
We worked with United Global Engineering Solutions for our industrial conveying needs, and the experience was excellent from start to finish. Their team quickly understood what we needed, recommended the right solution for our operations, and delivered high-quality industrial conveyor systems that made a real difference. Since installation, our workflow has improved and day-to-day operations are much more efficient. We truly value their support and would gladly recommend them.
Javier SánchezSatisfied Client 
We have worked with United Global on several projects, and their food-grade conveyor systems have delivered a significant improvement. What stands out most is their ability to customize solutions around our needs and deliver quality products on time. Their responsive support and cost-effective approach have made them a trusted partner.
Miguel TorresTrusted Partner 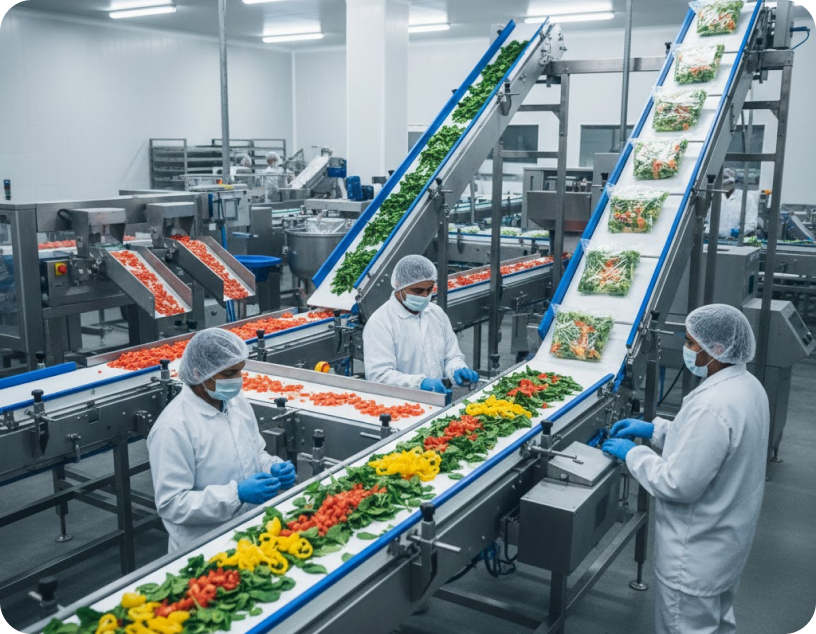
We have collaborated with United Global Engineering Solutions on multiple projects, and they have consistently delivered strong results. Their food-grade conveyor systems have brought a noticeable improvement to our operations, and we especially appreciate how they tailor each solution to our specific requirements. The team responds quickly, the service is efficient, and the solutions are cost-effective without compromising on quality.
Laura GómezHappy Manufacturer
- Industries Served
- 15+
- Years of Experience
- 10+
- Systems Installed
- 500+
- Happy Clients
- 600+