
Belt Conveyor System for Insulation Industry
UGES engineers belt conveyor systems for insulation manufacturers handling mineral wool, glass wool, and stone wool. Systems feature enclosed construction, static dissipation, and dust containment for lightweight fibrous materials.
Trusted by the largest brands
Belt Conveyor System Key Specifications

Belt Width

Belt Speed

Conveying Capacity

Maximum Incline Angle

Drive Power

Belt Type
Industrial Applications
Raw Material Batching and Furnace Feed
Proportioning belt conveyors feed weighed batches of basalt, dolomite, slag, and recycled material to the cupola or electric furnace for melting.
Post-Curing Oven Product Transport
Heat-resistant belt conveyors receive cured mineral wool blankets from the curing oven and transport them to cooling, trimming, and cutting stations.
Finished Product to Packaging Line
Low-speed wide-belt conveyors move cut insulation batts, rolls, and boards from the cutting line to compression packaging and palletizing systems.
What Our Partners Say
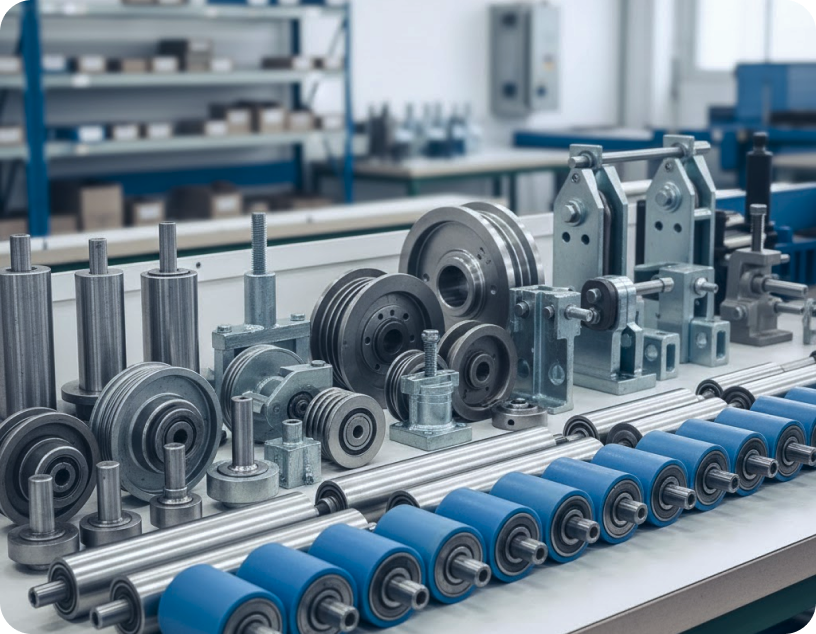
We have been sourcing material handling components from United Global Engineering Solutions for quite some time. Their conveyor accessories, including rollers and industrial pulleys, have consistently met our standards for quality and performance. We confidently recommend them for any conveyor system requirement.
Carlos MedinaRegular Client 
We worked with United Global Engineering Solutions for our industrial conveying needs, and the experience was excellent from start to finish. Their team quickly understood what we needed, recommended the right solution for our operations, and delivered high-quality industrial conveyor systems that made a real difference. Since installation, our workflow has improved and day-to-day operations are much more efficient. We truly value their support and would gladly recommend them.
Javier SánchezSatisfied Client 
We have worked with United Global on several projects, and their food-grade conveyor systems have delivered a significant improvement. What stands out most is their ability to customize solutions around our needs and deliver quality products on time. Their responsive support and cost-effective approach have made them a trusted partner.
Miguel TorresTrusted Partner 
We have collaborated with United Global Engineering Solutions on multiple projects, and they have consistently delivered strong results. Their food-grade conveyor systems have brought a noticeable improvement to our operations, and we especially appreciate how they tailor each solution to our specific requirements. The team responds quickly, the service is efficient, and the solutions are cost-effective without compromising on quality.
Laura GómezHappy Manufacturer
- Industries Served
- 15+
- Years of Experience
- 10+
- Systems Installed
- 500+
- Happy Clients
- 600+