
Comparaison de produits
Belt Conveyor vs Screw Conveyor — Choosing the Right System for Your Application
Belt conveyors and screw conveyors are two of the most common material handling systems in process plants, each suited to distinct application profiles. This comparison evaluates both technologies on the engineering criteria that determine the right selection for cement, power, mining, and chemical plant applications.
Plébiscité par les plus grandes marques
Belt Conveyor vs Screw Conveyor

Capacity & Throughput
- Belt Conveyor
- Belt conveyors handle high volumes efficiently — from 50 TPH to over 10,000 TPH depending on belt width and speed. They are the preferred choice for primary material transport where large tonnages must be moved continuously over extended periods.
- Screw Conveyor
- Screw conveyors are suited for low to moderate throughputs, typically up to 200–300 TPH for standard designs. They excel in metering, feeding, and controlled-rate material delivery applications where precise volume control is more important than peak capacity.

Conveying Distance
- Belt Conveyor
- Belt conveyors can transport material over distances ranging from a few metres to several kilometres with single or multiple drive arrangements. Long-distance overland conveyors with horizontal curves are standard in mining and cement plant raw material transport.
- Screw Conveyor
- Screw conveyors are practical for short distances — typically up to 30–40 metres for a single screw unit. Beyond this, power consumption rises sharply, shaft deflection becomes problematic, and multiple sections with intermediate bearings (hanger bearings) are needed, increasing maintenance complexity.

Material Characteristics
- Belt Conveyor
- Belt conveyors handle a wide range of materials from fine powders to large lumps, including abrasive, moist, and sticky materials with appropriate belt selection and transfer point design. They are less suitable for very hot materials without specialised heat-resistant belting.
- Screw Conveyor
- Screw conveyors are ideal for fine to granular free-flowing materials and can also handle semi-fluid and sluggish materials with modified flight designs (ribbon, paddle, or cut flights). They can handle hot materials up to 400°C with appropriate trough and screw construction.

Dust Containment & Sealing
- Belt Conveyor
- Belt conveyors are open systems that require additional covers, wind boards, and transfer point enclosures for dust control. Achieving effective sealing adds cost and maintenance complexity, particularly at loading and discharge points.
- Screw Conveyor
- Screw conveyors are inherently enclosed, providing excellent dust containment without additional equipment. This makes them preferable for handling hazardous, toxic, or hygroscopic materials where environmental isolation is a regulatory or process requirement.

Power Consumption
- Belt Conveyor
- Belt conveyors are energy-efficient for high-volume, long-distance applications due to low friction coefficients and optimised drive systems. Power consumption per tonne-kilometre is typically the lowest among mechanical conveying methods.
- Screw Conveyor
- Screw conveyors consume relatively more power per tonne of material moved due to friction between the material, screw flights, and trough. Power consumption increases disproportionately with conveying length and material bulk density, making them less efficient for high-tonnage applications.
Faire le bon choix
Quand choisir Belt Conveyor
Choose belt conveyors for high-capacity, long-distance material transport — limestone from quarry, clinker from cooler to storage, coal handling, and any application exceeding 300 TPH or 40 metres conveying length. They are the backbone of bulk material handling in heavy industries.
Quand choisir Screw Conveyor
Choose screw conveyors for short-distance, enclosed conveying of fine or granular materials — cement feeding, fly ash handling, chemical dosing, and silo discharge. They are ideal when dust containment, metering accuracy, or handling of hot materials are primary requirements.
Notre recommandation
Both conveyor types are essential in a well-designed plant, serving complementary roles. UGES manufactures both belt conveyor systems (with precision-engineered idlers and pulleys) and screw conveyors (with hardened flights and precision-machined shafts). Our engineering team can help you select and size the right system based on your specific material, capacity, and layout requirements.
Témoignages de réussite client
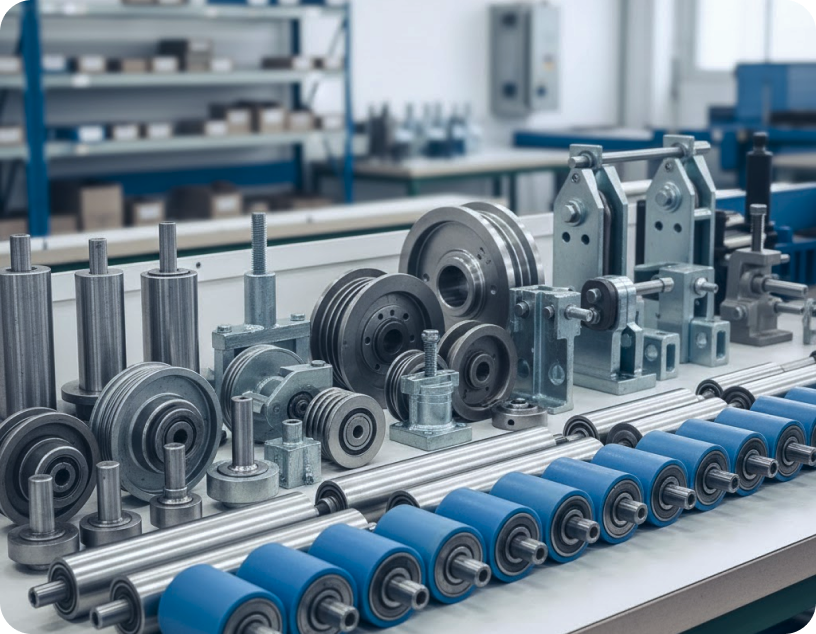
Nous nous approvisionnons en composants de convoyage auprès de United Global Engineering Solutions depuis déjà un certain temps. Leurs accessoires pour bandes transporteuses, notamment les rouleaux et les poulies industriels, ont toujours répondu à nos exigences en matière de qualité et de performance. Nous les recommandons vivement pour tous vos besoins en systèmes de convoyage.
Mathieu BernardLe client fidèle 
Nous avons travaillé avec United Global Engineering Solutions pour nos besoins en convoyage, et l’expérience a été excellente du début à la fin. Leur équipe a rapidement compris nos exigences, nous a recommandé la solution de convoyage la plus adaptée à notre activité et a livré des bandes transporteuses industrielles de qualité qui ont réellement fait la différence. Depuis l’installation, notre flux de travail s’est amélioré et les opérations quotidiennes sont beaucoup plus efficaces. Nous leur sommes reconnaissants pour leur accompagnement et les recommandons sans hésiter.
Julien MoreauLe client satisfait 
Nous avons travaillé avec United Global sur plusieurs projets, et leurs bandes transporteuses pour l’industrie agroalimentaire ont vraiment fait la différence. Ce qui se démarque le plus, c’est leur capacité à adapter les solutions à nos besoins et à livrer des produits de qualité dans les délais. Leur réactivité et leur approche économique en font un partenaire sur lequel nous pouvons compter.
Nicolas LaurentLe partenaire de confiance 
Nous avons travaillé avec United Global Engineering Solutions sur plusieurs projets, et ils ont toujours été à la hauteur. Leurs bandes transporteuses pour l’industrie agroalimentaire ont vraiment fait la différence pour nous, et nous avons particulièrement apprécié leur capacité à adapter leurs solutions à nos besoins spécifiques. L’équipe est réactive, le service est rapide, et les solutions sont économiques sans compromis sur la qualité.
Antoine DuboisLe fabricant satisfait
- Secteurs desservis
- 15+
- Années d'expérience
- 10+
- Systèmes installés
- 500+
- Clients satisfaits
- 600+