
Problème et solution
Rotary Airlock Valve Air Leakage - Root Causes & Engineered Solutions
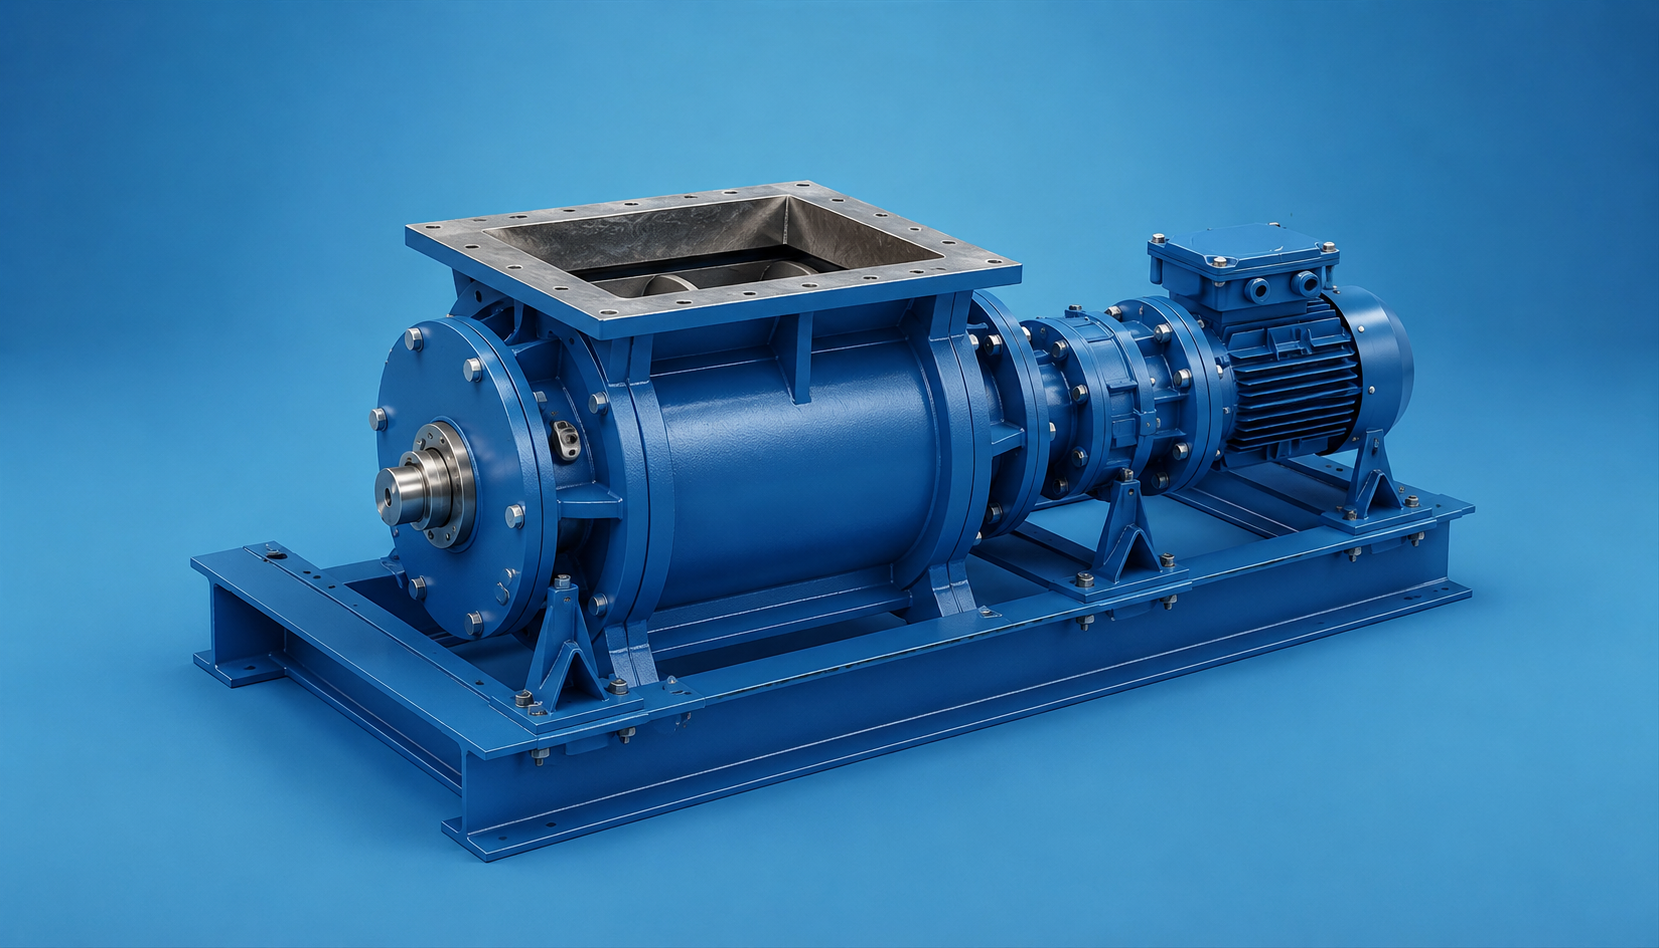
Rotary airlock valve air leakage is a common, overlooked cause of lost conveying capacity and fugitive dust in cement, power, and chemical plants. As rotor tips and the housing bore wear, the running clearance opens past 0.5 mm and air leaks across the valve, cutting efficiency by 20 to 40% and pushing dust past compliance limits. UGES hard-faced airlock valves restore and hold the seal.
Plébiscité par les plus grandes marques
Comprendre Rotary Airlock Valve Air Leakage

Description du problème

Coût de l’inaction
Causes profondes
Rotor-Tip and Housing Bore Wear from Abrasive Media
Fine, abrasive products like cement, fly ash, and clinker dust act as a grinding medium between the rotor tips and the housing. Standard mild-steel or untreated rotors lose their sharp tip geometry within months, and the housing bore wears oval, opening the running clearance well beyond the 0.1–0.2 mm needed for an effective seal. Because leakage scales sharply with clearance, even 0.3–0.5 mm of wear can double or triple air loss across the valve.
Excessive Pressure Differential and Material Blowback
When the pressure differential across the valve is higher than the rotor pocket and venting were designed for, air escapes upward through the incoming material, fluidizing it and causing "blowback" that prevents pockets from filling completely. The valve then meters less material per revolution while leaking more air — a double hit to efficiency. Un-vented or under-vented inlets and oversized pockets make this worse, especially with light, aeratable powders.
Seal/Bearing Contamination and Thermal Effects
Without effective shaft seals and bearing protection, product migrates along the shaft into the end covers and bearings, contaminating grease and driving premature bearing failure that lets the rotor drift and rub. In high-temperature duty — kiln, clinker-cooler, and ESP-hopper applications — inadequate thermal clearance causes the rotor to expand against the housing and seize, while heat degrades standard seals and lubricants not rated for the service.
Solutions d'ingénierie
Hard-Faced, Adjustable-Tip Rotary Airlock Valves
UGES airlock valves use hardened, hard-faced rotor tips (chrome-carbide overlay, Ni-Hard, or tungsten-carbide coating) running in a wear-lined or hard-chromed housing, so the sealing geometry survives abrasive service far longer. Adjustable or replaceable tip strips let the clearance be reset in the field to under 0.15 mm without scrapping the rotor — sustaining volumetric sealing efficiency above 95% over a multi-year service life instead of degrading within months.
Vented, Reduced-Pocket Valve Design
For high-differential and light-powder duty, UGES supplies airlock valves with engineered inlet venting and shrouding, reduced or shallow rotor pockets, and chamfered tips that relieve trapped air and stop blowback. This restores consistent pocket fill and stabilizes feed, recovering metering accuracy and conveying capacity while cutting the air carried back up through the material stream.
High-Temperature, Purged-Bearing Valves & Clearance Service
For kiln, clinker-cooler, and ESP service, UGES builds airlock valves with outboard bearings isolated from the product, shaft air-purge or gland-packed seals, and increased thermal running clearances that prevent rotor seizure as components expand. UGES also supports plants with periodic tip-clearance inspection and rotor-tip replacement, catching leakage early and keeping valves at peak sealing efficiency between shutdowns.
Témoignages de réussite client
Nous nous approvisionnons en composants de convoyeurs auprès de United Global Engineering Solutions depuis un bon moment déjà. Leurs accessoires pour bandes transporteuses, notamment les rouleaux et poulies de convoyeur industriels, ont toujours répondu à nos exigences de qualité et de performance. Nous les recommandons vivement pour tous vos besoins en systèmes de convoyage.
Mathieu BernardLe client fidèle 
Nous avons travaillé avec United Global Engineering Solutions pour nos besoins en convoyeurs, et l’expérience a été excellente du début à la fin. Leur équipe a rapidement compris nos exigences, nous a recommandé la solution de convoyage adaptée à nos opérations et a livré des bandes transporteuses industrielles de qualité qui ont réellement fait la différence. Depuis l’installation, notre flux de travail s’est amélioré et les opérations quotidiennes nous paraissent bien plus efficaces. Nous leur sommes reconnaissants pour leur soutien et les recommandons sans hésiter.
Julien MoreauLe client satisfait 
Nous avons travaillé avec United Global sur plusieurs projets, et leurs bandes transporteuses pour l’industrie agroalimentaire ont fait une réelle différence. Ce qui se démarque le plus, c’est leur capacité à personnaliser les solutions selon nos besoins et à livrer des produits de qualité dans les délais. Leur service réactif et leur approche rentable en font un partenaire sur lequel nous pouvons compter.
Nicolas LaurentLe partenaire de confiance 
Nous avons travaillé avec United Global Engineering Solutions sur plusieurs projets, et ils ont toujours répondu présents. Leurs bandes transporteuses pour l’industrie agroalimentaire ont véritablement changé les choses pour nous, et nous avons apprécié leur capacité à adapter les solutions à nos besoins spécifiques. L’équipe est réactive, le service est rapide et les solutions sont économiques sans compromettre la qualité.
Antoine DuboisLe fabricant satisfait
- Secteurs desservis
- 15+
- Années d'expérience
- 10+
- Systèmes installés
- 500+
- Clients satisfaits
- 600+
Résolvez Rotary Airlock Valve Air Leakage avec UGES
Nos experts se rendent sur votre site, comprennent votre flux de travail et recommandent la configuration exacte dont votre système a besoin.